
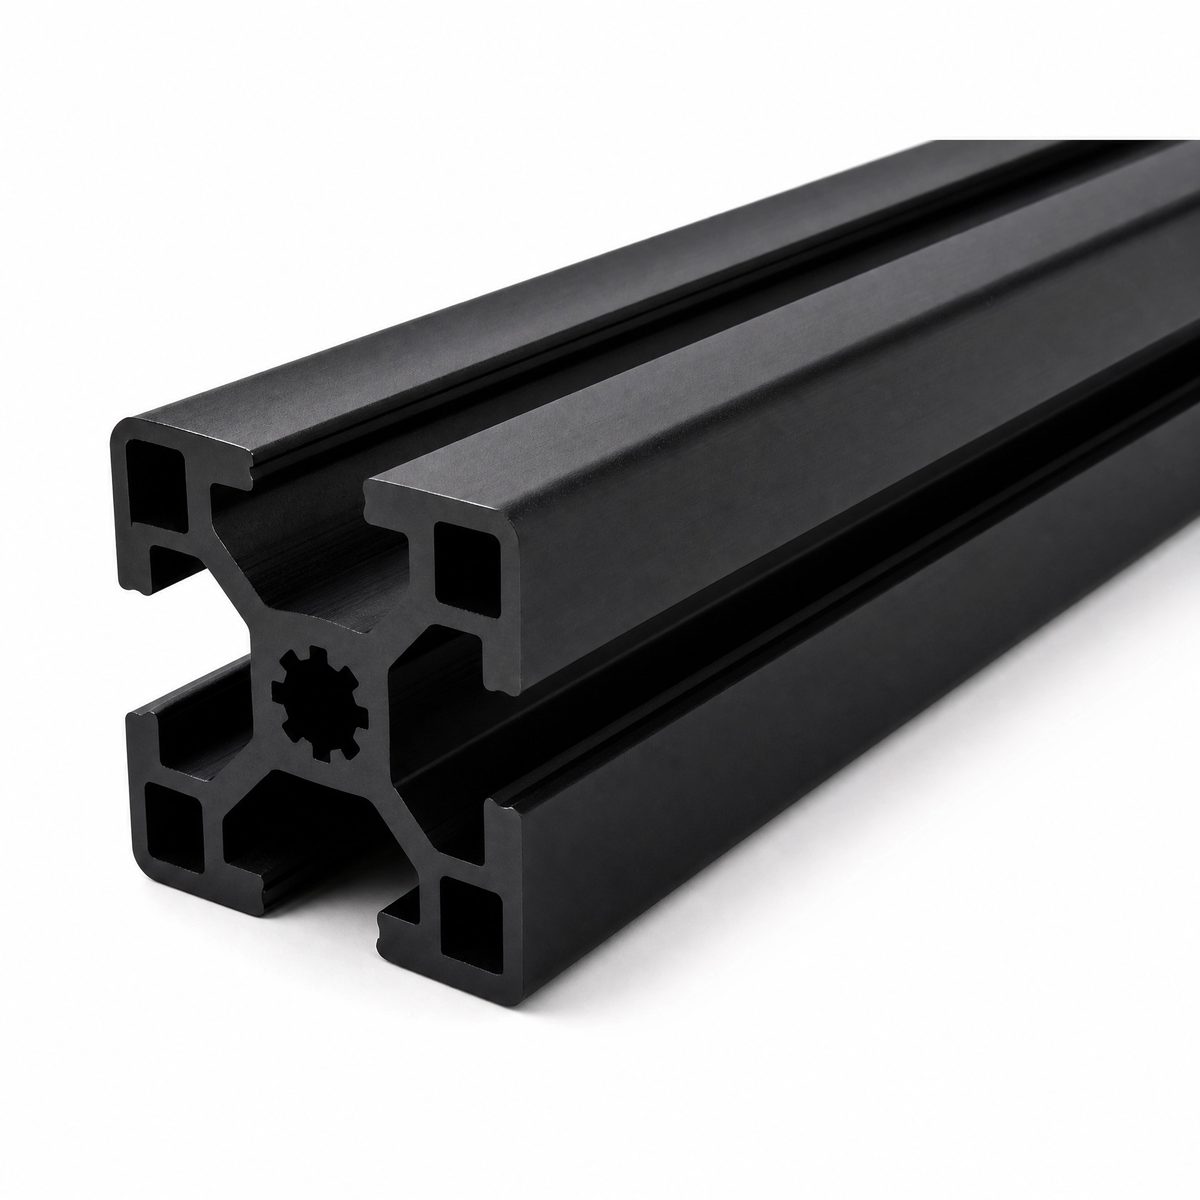
Custom Aluminum Profiles
Eloxiertes Aluminiumprofil
Eloxierte Aluminiumprofile in 5-25 µm bei 200-300 HV, in Silber, Champagner, Bronze, Schwarz oder Gold. Elektrolytfarbe, versiegelt, Dicke nach Zeichnung vereinbart.
Produktdetails
Kurze Antwort: anodizing converts the outer few microns of the aluminum into a hard oxide layer that is part of the metal, then seals the pores so it stops absorbing. We run 5–25 µm on 6063 and 6061, at 200–300 HV, in silver, champagne, bronze, black or gold, with matte, brushed, polished or sandblasted texture underneath. Film thickness and color are set against your drawing and your sample: 10–15 µm covers most indoor work, 20–25 µm is what outdoor and industrial parts need, and we confirm the achievable range before the parts go into the bath.
What the film actually is
Anodizing is an electrochemical conversion, not a coating. The profile is made the anode in a sulfuric acid electrolyte and current is passed through it, so the surface aluminum becomes aluminum oxide. Because the oxide grows out of the metal, it cannot delaminate the way paint or plating can. What it can do is crack, if the part is bent after coating, which is why forming always happens first.
The film has two layers and the distinction matters. Next to the metal is a thin, dense barrier layer that does the real corrosion protection. Above it is a porous layer, a honeycomb of hexagonal cells running outward from the barrier. That porous structure is what makes coloring possible, because dye and metal salts can be driven down into the pores, and it is also why an unsealed anodized part is a liability: the pores are open, so they absorb oil, fingerprints and contamination, and the corrosion resistance is a fraction of what the same film gives once sealed.
Sealing closes those pores, usually by boiling the part in deionized water or a hot nickel-acetate bath, which swells the oxide and plugs the openings. It is the step that decides whether a 15 µm film lasts five years outdoors or one. When a supplier quotes anodizing without mentioning sealing, the number being quoted is only half a process.
Spezifikationen
| Element | Bereich |
|---|---|
| Prozess | Sulfuric-acid anodizing, electrolytic or dye coloring, high-temperature sealing |
| Schichtdicke | 5–25 µm, selected by service environment; confirmed against your drawing |
| Oberflächenhärte | 200–300 HV |
| Farben | Natural silver, champagne, bronze, black, gold |
| Oberflächentextur | Matte, brushed, polished, sandblasted, all under the anodized film |
| Legierungen | 6063-T5, 6061-T6; 6-series gives the clearest, most uniform film |
| Maximale Teilelänge | 6,500 mm |
| Electrolyte temperature | 19–21 °C |
| Sulfuric acid concentration | 50–65 g/L |
| Current density | 130–150 A/m² |
| Sealing | High-temperature sealing after coloring |
| Referenznorm | GB/T 5237.2-2017, ISO 7599 |
| Prüfung | Film thickness reported per batch; salt-spray results on request |
Choosing a color, and why the choice holds
Anodized color is not paint, and it does not sit on the surface. Two different mechanisms are in play, and they age differently.
- Electrolytic coloring deposits metal salts at the base of the pores, so the color is inside the film. Silver, champagne, bronze and black are normally made this way. The finish keeps the metallic depth of aluminum and does not fade in sunlight, because there is no organic dye to break down.
- Chemical dyeing fills the pores with an organic dye. It reaches colors electrolytic coloring cannot, such as red or blue, but it is sensitive to UV. For an indoor part that is fine; for a south-facing facade it is the wrong choice.
Texture is decided before any of this, because it is cut or blasted into the metal rather than added on top. Sandblasting gives a diffuse, low-glare surface that hides handling marks. Brushing leaves directional lines and reads as machined. Polishing produces the brightest finish and also the least forgiving, since every scratch in the base metal shows through. Matte sits between polished and sandblasted and is the usual choice for equipment frames where glare is a nuisance.
One point worth knowing before specifying a color on a drawing: anodized film is transparent, so the alloy and the extrusion surface are visible through it. A die line or a weld will still be there after anodizing, slightly softened but not hidden. If a part has to look uniform regardless of what is underneath, powder coating is the process that covers, and anodizing is not.
Anodizing against hard anodizing and powder coating
| Eigenschaft | Anodizing | Hard anodizing | Powder coating |
|---|---|---|---|
| Schichtdicke | 5–25 µm | ≥ 25 µm; 50–80 µm standard | 60–120 µm |
| Hardness | 200–300 HV | HV ≥ 350; 400–600 typical | 2H–4H pencil |
| Color range | Silver, champagne, bronze, black, gold | Gray-brown to black only | Full RAL and Pantone |
| Look | Metallic, substrate visible through film | Functional, dark | Opaque, covers the substrate |
| Dimensional change | Small, roughly half the film thickness | Significant, roughly half the film thickness | Large, and it adds in one direction only |
| Best use | Appearance plus moderate wear | Sliding wear, insulation, heat | Brand color, outdoor architecture, covering defects |
The practical line between them: if the part has to look like metal, anodize it. If it has to survive contact, hard anodize it. If it has to be a specific color or hide what is underneath, powder coat it.
How the process is controlled
Three stages, and each one can ruin the result on its own.
- Pre-treatment. Degreasing, then alkaline etching, then neutralization. This removes oil and the natural oxide so the anodizing current sees clean metal. Skip it or run it badly and the film comes out patchy, with visible streaks that no amount of sealing will hide.
- Anodizing. 19–21 °C electrolyte, 50–65 g/L sulfuric acid, 130–150 A/m². Temperature is the variable that decides color consistency: drift a couple of degrees between batches and the same nominal color comes out two different shades.
- Coloring and sealing. Electrolytic or dye coloring, then high-temperature sealing. Sealing is what locks the color in and closes the pores.
Alloy choice interacts with all of this. 6063 and 6061 anodize to a clear, even film because they have little copper and silicon in solid solution. Alloys with more copper, such as the 2xxx and 7xxx families, anodize to a darker, grayer film that cannot be brought back to silver, which is why a drawing that specifies both 7075 and a bright silver finish needs correcting before production.
Wo dies passt
- Equipment frames and machine guards that have to look finished and resist handling wear
- Architectural trim, handrails and window sections where the metallic look is the point
- Instrument and electronics housings in black, where a low-glare, non-conductive finish is wanted
- Parts that need corrosion resistance without adding a measurable coating thickness, such as close-tolerance extrusions
- Anywhere a brushed or sandblasted texture should read as machined metal rather than painted
Wo es nicht passt
- A part that must be red, blue, green or any color outside the anodizing range. Those colors come from dye and will fade outdoors.
- A part with visible die lines, weld seams or scratches that have to disappear. The film is transparent and will not hide them.
- A part that is bent or welded after coating. Bend and weld first; anodizing is the last step.
- Heavy sliding contact under load, where 200–300 HV is not enough and hard anodizing is the correct process.
Was für ein Angebot zu senden ist
- The drawing, with the alloy and temper stated, since the alloy decides the achievable color
- The color, referenced to a physical sample or a RAL code where possible
- The required texture: matte, brushed, polished or sandblasted
- The service environment, indoor or outdoor, which sets whether 10 µm or 25 µm is appropriate
- Surfaces that must stay bare, such as electrical contact points or machined fits
- Menge und die längste Einzellänge, geprüft gegen die 6.500-mm-Grenze
If the color is not settled, send a photograph of a part you already use, or a sample. Matching to a physical sample is far more reliable than matching to a screen.
FAQ
What film thickness should I specify?
Match it to the environment rather than to a maximum. 5–10 µm suits indoor decorative parts that see little handling. 10–15 µm is the general-purpose band for equipment and enclosures. 20–25 µm is what outdoor exposure and industrial wear call for. Above that the film gets harder but also more brittle, and it cracks at tight bends and sharp corners. As a reference we run within these bands and confirm the achievable value for your part before production.
Will anodizing change my dimensions?
By roughly half the film thickness per surface, outward. At 15 µm that is around 7–8 µm per face, which is usually inside the tolerance of an extruded profile. On a machined bore or a shaft that runs in a bearing it is not negligible, so those dimensions need the allowance written in. Tell us which dimensions are critical and the allowance is set against them.
Does anodized color fade in sunlight?
Electrolytic colors such as champagne, bronze and black do not fade in any practical sense, because the color is metal deposited inside the film rather than an organic dye. Dyed colors, which is how bright reds and blues are made, are UV-sensitive and will shift outdoors over years. For an outdoor part, stay within the electrolytic range.
Can you match a color from a previous batch?
Within a batch, yes: bath temperature and concentration are held to keep the shade consistent. Across batches, a small shift is normal in any anodizing line, because the alloy heat, the bath age and the sealing all move the final tone slightly. For repeat orders we keep the reference sample and match against it, and where the color is critical we send a coated sample for approval before the run.
Can you anodize 7075 or 2024?
We can, but the result will not be silver. High-copper alloys produce a darker, grayer film that cannot be brought back to a bright metallic tone. If the drawing pairs 7075 with a natural-silver finish, one of the two has to change, and we raise that at quotation stage rather than after coating.
What is the longest part you can anodize?
6,500 mm. Longer extrusions are split at a joint the design already needs, coated as separate lengths and assembled afterwards. If a continuous length is essential, that constraint needs to be known before the profile is designed, not after it is extruded.
Senden Sie Ihre Zeichnung
Email linjunbing@truetrustlv.com with the drawing, the alloy and the color reference. If the color is still open, send a photograph or a sample of what you already use and we will match against it. You will get a process proposal, a quotation and the film thickness we can hold — reviewed by an engineer, not an auto-reply.
WhatsApp: +86 136 6644 0600
ANGEBOT ERHALTEN
Sobald Sie Ihre Anforderungen übermittelt haben, kontaktieren wir Sie so schnell wie möglich bezüglich Ihrer Produktanfrage.:Eloxiertes Aluminiumprofil