
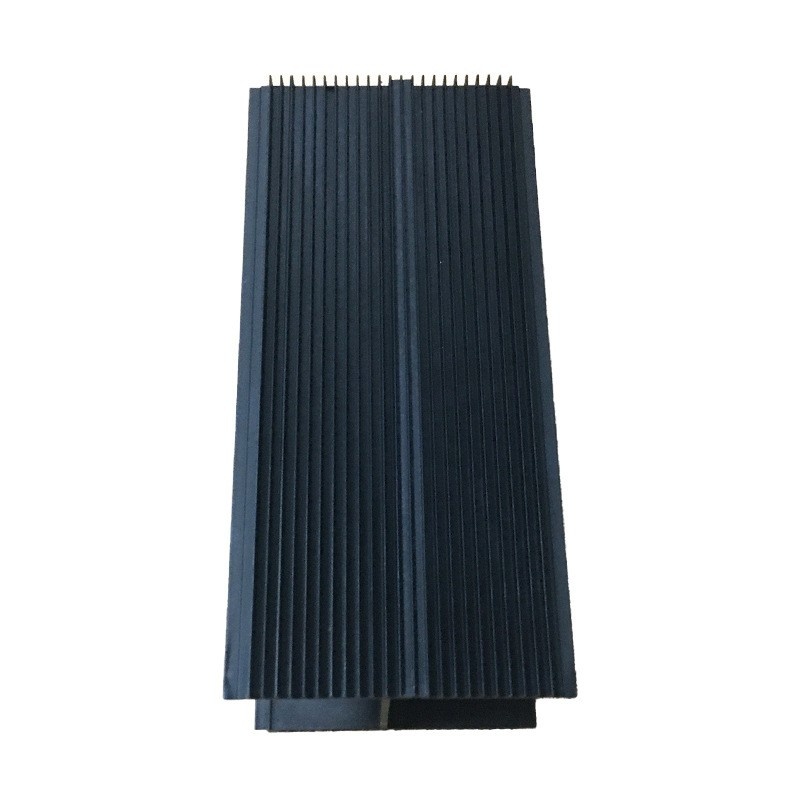
Aluminum profiles for radiators
High Thermal Conductivity Pure Aluminum Heat Sink Profiles
High conductivity heat sinks in 1070 pure aluminum at 226 W/m-K, fins to 0.5 mm and 15:1 aspect ratio, flatness 0.05 mm per 100 mm. Per drawing.
Produktdetails
Kurze Antwort: a high-conductivity pure aluminum heat sink is extruded from the 1070 series at about 226 W/m·K, roughly 12 percent above 6063 at 201 W/m·K. That 12 percent only reaches the part when the bottleneck is conduction. The bigger gain is usually that pure aluminum extrudes thinner fins at a higher aspect ratio, which buys surface area on the convection side. Working reference: 0.5 mm minimum fin thickness, 15:1 fin height to thickness. Section and tolerance per your drawing.
Wofür es verwendet wird
It goes where the thermal design space is tight and the power density is high: high-power LED arrays, laser diode and fiber laser bodies, industrial power supplies, traction and charging power modules, communication radio heat sinks, and any package where the heat has to be spread sideways before it can be removed.
These are the cases where the enclosure is already fixed by something else. The board size, the connector positions and the mounting points are decided, and the thermal engineer has a few millimeters of height to work with. That is when material conductivity stops being a datasheet comparison and starts being a design variable.
Spezifikationen
| Element | Arbeitsreferenz | Wie es festgelegt wird |
|---|---|---|
| Legierung | 1070 pure aluminum, 99.7 percent or higher | Gewählt nach Ihrem Lastfall |
| Wärmeleitfähigkeit | 226 W/m·K on 1070, 201 W/m·K on 6063-T5 | Materialeigenschaft, durch Legierung festgelegt |
| Minimum fin thickness | 0.5 mm | Set by your drawing and the extrusion ratio |
| Fin aspect ratio | Up to 15:1 | Durch Ihre Zeichnung festgelegt |
| Fin thickness tolerance | ±0.03 mm | Durch Ihre Zeichnung festgelegt |
| Grundebenheit | ≤0.05 mm per 100 mm | Durch Ihre Zeichnung festgelegt |
| Oberfläche | Anodized, clear or black, or conversion coated | Set by your corrosion and emissivity target |
| Bearbeitung | Milling, drilling, tapping, precision cut | Nach Ihrer Schnittstellenzeichnung |
Wie es hergestellt wird
- The billet is extruded through a die shaped for the fin geometry. Pure aluminum flows more easily than an alloy, which is what makes the thin, tall fin possible in the first place.
- The section is cut and the base machined flat, with holes and mounting features machined on the same datum as the mating face.
- Where threads are needed in a soft material, the drawing is reviewed for inserts or a local increase in wall thickness rather than a thread cut straight into 1070.
- Anodizing follows if required, with masked areas where the part needs electrical or thermal contact on bare metal.
- Inspection checks fin thickness, aspect ratio and flatness on the finished part.
Wo dies passt
It fits when conduction spreading is a real part of the thermal budget, when the fin geometry has to be thin or tall, and when the part is supported by something else so the soft material is not carrying the load.
Wo es nicht passt: if the bottleneck is the air side, changing alloy buys very little and a larger or better-shaped section buys much more. If the heat sink is also a structural member, 6063 or 6061 is the right answer and 1070 is a false economy. And if the part has to take repeated threaded assembly, plain 1070 will strip.
The honest version of the 12 percent
Thermal resistance in a real assembly is a chain: through the base, across the interface, then out of the fins into the air. Only the first link is improved by a better alloy. When the convection link dominates, which it does on most natural-convection parts, cutting the conduction link by 12 percent changes the total by a few percent. That is real, and it is not the step change that a datasheet comparison suggests.
So the useful question is not "which alloy conducts more" but "where is the resistance". If the base is long and thin and the heat source is small, conduction spreading dominates and 1070 genuinely earns its place. If the base is short and the fins are large, the air is the limit and the alloy is nearly irrelevant.
Where pure aluminum actually wins is formability. 1070 flows better than 6063, so a die can carry thinner and taller fins: 0.5 mm thickness at up to 15:1 aspect ratio. That adds surface area inside the same envelope, and surface area acts directly on the convection link that was the bottleneck. In practice the area gain usually matters more than the 12 percent, and it is the reason we ask what the fin geometry needs to be before discussing alloy.
The cost is strength, and it is not negotiable. 1070 is soft. Threads strip, clamped faces deform, and a part that is expected to hold a module flat will not do it if the material creeps under clamp load. The fixes are real and cheap when designed in: inserts at thread locations, a thicker base under the clamp, ribs, or a 6063 frame carrying the load with a 1070 spreader inside it. What does not work is specifying 1070 for a structural housing and discovering it at assembly. Hard anodizing also does less for a soft substrate than for an alloy, because the film follows the substrate and a dent goes straight through it.
Was für ein Angebot zu senden ist
- The section drawing with fin thickness, fin height and base thickness dimensioned
- Heat load, the size of the source, and whether the budget is conduction or convection limited
- Whether the part carries structural or clamping load, and where threads fall
- Surface and finish requirement
- Quantity per year, since the die geometry and the alloy choice interact
FAQ
What tolerance can you hold on a pure aluminum heat sink?
Fin thickness within ±0.03 mm and base flatness at or under 0.05 mm per 100 mm are our reference values on this family. The value on your order is set by your drawing, and we confirm it in writing before quotation. On very thin, very tall fins the achievable band tightens with the aspect ratio, so we state the limit for the geometry you send rather than a generic figure.
Why is 1070 more conductive than 6063?
Because conductivity falls as alloying elements are added. 1070 is 99.7 percent aluminum or better, while 6063 carries magnesium and silicon at around 1.5 percent total. Those additions give 6063 its strength, and they also scatter electrons, which is exactly what lowers conductivity. The two properties trade against each other and cannot both be maximized.
Is 12 percent conductivity worth changing material for?
Only where conduction is the limiting link. On a short base with large fins the air dominates and the gain is diluted to a few percent on total thermal resistance. On a long thin base with a small source, it is worth having. We will tell you which case yours is, including when the answer is that you should keep 6063.
Can I put threads directly in 1070?
You can, and they will strip under repeated assembly. On this material we recommend inserts or a local wall increase at the thread locations, and we will raise it at drawing review. Silent thread failure in the field is worse than a small cost at machining.
What surface treatments suit pure aluminum?
Anodizing works well and gives a uniform, bright film because the substrate is homogeneous, which is why 1070 is also used for appearance parts. Black anodizing adds emissivity where radiation matters. The limitation is mechanical rather than chemical: the substrate is soft and scratches easily, so handling protection matters more than on an alloy part.
Does pure aluminum weld better?
Yes, it welds readily, which can be useful when a base plate or a boss has to be joined on. That said, a welded joint in the heat path is still a joint, so where the geometry allows we would rather form the feature in the extrusion than add it afterwards.
Nächster Schritt
Send the section drawing with the fin geometry and the heat load, and tell us whether the part carries load. We will come back with a proposed alloy, a die concept and a written tolerance statement against your drawing.
E-Mail: linjunbing@truetrustlv.com | Anrufen oder WhatsApp: +86 136 6644 0600
ANGEBOT ERHALTEN
Sobald Sie Ihre Anforderungen übermittelt haben, kontaktieren wir Sie so schnell wie möglich bezüglich Ihrer Produktanfrage.:High Thermal Conductivity Pure Aluminum Heat Sink Profiles