
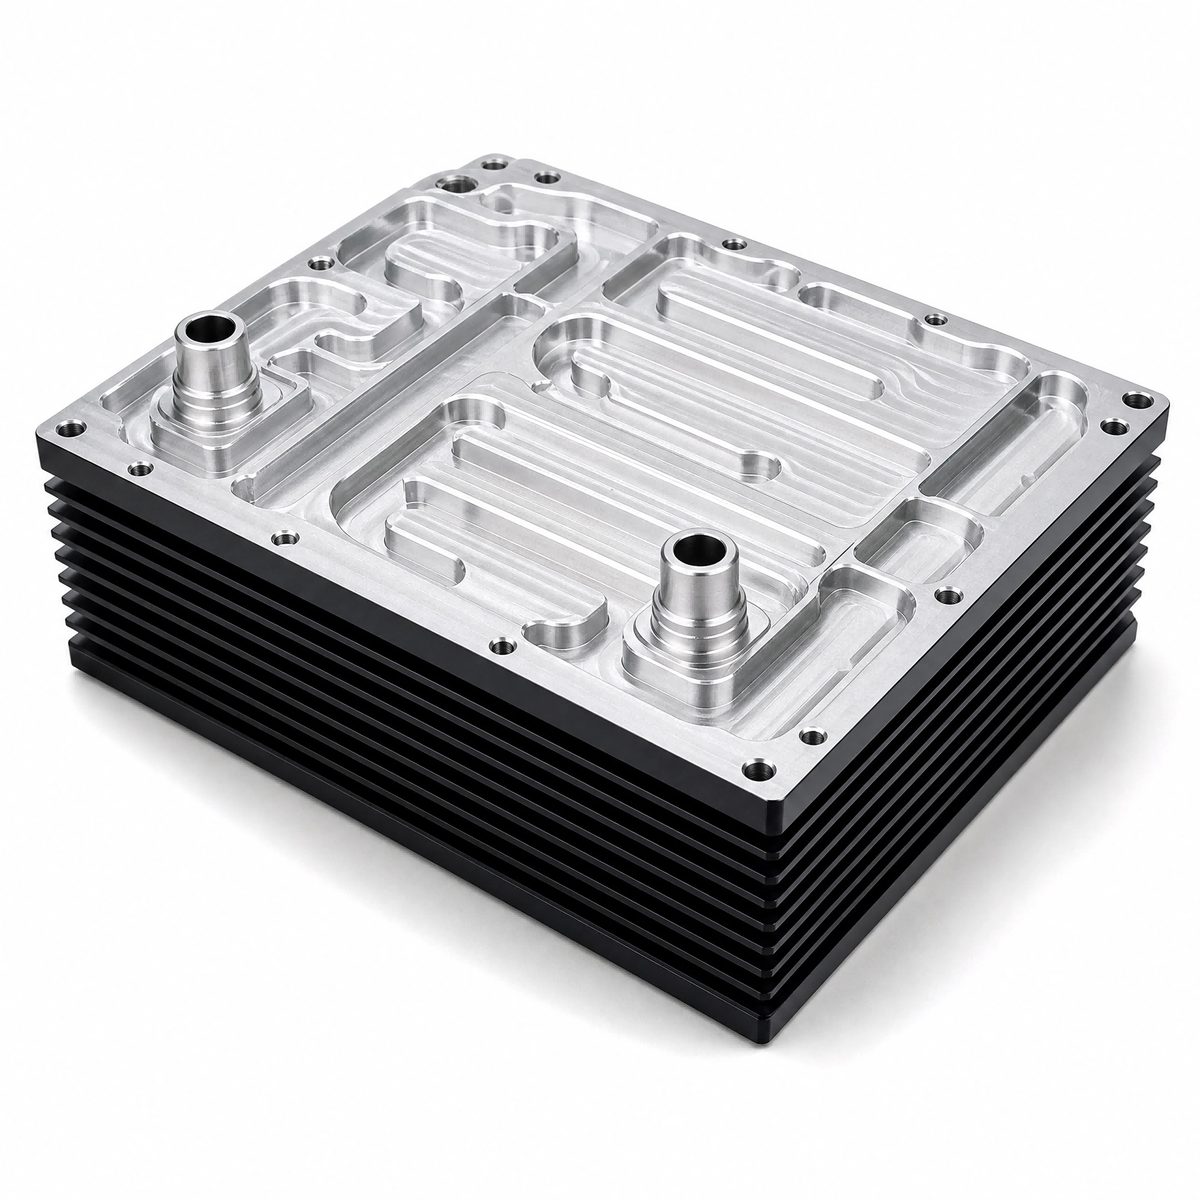
Aluminum profiles for radiators
Kühlkörpergehäuse-Aluminiumprofil für Motorsteuerung
Kühlkörpergehäuse für Motorsteuerung: extrudiertes 6063-T5 bei 201 W/m-K, bearbeitet auf +/-0,01-0,005 mm, IP67 bis IP6K9K, hart eloxiert. Nach Zeichnung.
Produktdetails
Kurze Antwort: a motor controller heat sink housing is an extruded aluminum body that carries the IGBT or SiC module, conducts its heat out through integrated fins or a water channel, and closes into a sealed cavity that meets the vehicle's IP requirement. It is three parts in one: heat sink, structure and enclosure. Working reference: 201 W/m·K on 6063-T5 against roughly 96 W/m·K on die casting, machined features at ±0.01–0.005 mm. Section, sealing and tolerance are set by your drawing.
Wofür es verwendet wird
It sits at the heart of the traction inverter on battery electric and hybrid vehicles, and on the motor controller of electric drives in industrial vehicles, marine drives and high-power pumps. The module inside switches hundreds of amps, and its junction temperature is the limit that decides how much current the controller can deliver.
The consequence of getting it wrong is specific. Once the junction passes about 150 °C, switching efficiency falls by more than 30 percent, and past that point thermal runaway can destroy the module rather than merely derate it. So the housing is not packaging around the electronics. It is the part that sets the current rating.
Two build types dominate. Air cooled housings form dense internal fins, down to about 0.5 mm fin thickness, with an external fan for forced convection. Water cooled housings carry a channel through the section, either serpentine or multi-channel parallel, and handle far higher heat flux in the same envelope.
Spezifikationen
| Element | Arbeitsreferenz | Wie es festgelegt wird |
|---|---|---|
| Legierung | 6063-T5, about 201 W/m·K | Chosen against your load and strength case |
| Rippenstärke | Down to 0.5 mm | Set by your drawing and the extrusion ratio |
| Bearbeitungsgenauigkeit | ±0.01–0.005 mm on critical features | Durch Ihre Zeichnung festgelegt |
| Sealing groove | Machined on the end face, O-ring or sealant compatible | Per your cap design and the IP target |
| Schutz | IP67, up to IP6K9K with the right cap and fastening | Set by the vehicle specification |
| Oberfläche | Hard anodizing for insulation and wear | Set by the voltage platform and your drawing |
| Channel type | Serpentine or multi-channel parallel | Chosen against your pressure drop and flow |
| Test | Leak test before finish on water-cooled bodies | Set by your acceptance standard |
Wie es hergestellt wird
- The body is extruded with the fins or the channel formed in the section, so the heat path from the module seat to the coolant has no bonded joint.
- End faces are milled flat and square. On a sealed housing this is the step that decides whether the O-ring compresses evenly, and it is where most sealing problems actually originate.
- Sealing grooves, mounting holes, module seats and water inlet and outlet ports are machined, typically on five-axis equipment, on a datum tied to the module seat.
- Water-cooled bodies are leak tested before any coating, because a coating can hide a weep and a leak found after assembly is a scrap event.
- Hard anodizing follows, with threads and grounding pads masked so that electrical contact does not depend on a coating.
Wo dies passt
It fits when the controller has a constant cross-section along its length, when the module seat can be machined flat, and when the cavity can be closed by end caps rather than by a complex three-dimensional shell.
Wo es nicht passt: if the housing has to branch, curve or change section along its length, a die casting or a machined billet is the right process and we will say so. If the volume is a handful of units, the die is not worth it. And if the requirement is a sealed cavity with no external fin face at all, the thermal path has to be redesigned rather than quoted.
Three things that decide whether this part works
Extrusion versus die casting is not a conductivity contest, it is a porosity question. The numbers usually quoted are 201 against 96 W/m·K, which makes the choice look obvious. The real difference is that a die casting carries gas porosity, and porosity sitting in the heat path is a local resistance that varies from part to part. An extrusion is wrought and homogeneous, so its thermal behaviour repeats. Die casting still wins where the shape is genuinely three-dimensional. Where the housing is a constant section, the extrusion is both cooler and more consistent.
Sealing is a flatness problem before it is a gasket problem. IP67 means dust tight and short-term immersion, and IP6K9K means it survives a high-pressure, high-temperature jet. Both are achieved at the end face, where the cap compresses an O-ring or a sealant bead. If the extruded end face is not milled flat, the compression varies around the perimeter, and the leak appears at the point of least compression under vibration rather than on the test bench. This is why we machine the end face rather than trusting the cut.
Hard anodizing is insulation, but it is not a substitute for clearance. On a 300 to 800 V platform the coating does real electrical work, and it also gives wear resistance at the mounting faces. What it does not do is guarantee a withstand voltage at a sharp corner or inside a thread, because the film thins there and the coating is porous by nature. The design has to leave creepage distance and keep high-voltage contact on masked, bare surfaces. A drawing that relies on the coating alone for isolation is a drawing we will query before quoting.
Was für ein Angebot zu senden ist
- The housing drawing with the module seat, the sealing face and the port positions dimensioned
- Heat load in watts, coolant flow and inlet temperature, or the airflow if air cooled
- Voltage platform, because it drives the insulation requirement
- The IP rating and the test method used to verify it
- Cap and fastener design, or the interface the cap has to mate with
FAQ
What machining tolerance can you hold?
±0.01 to 0.005 mm on critical machined features such as the module seat and the sealing groove, with base flatness typically held to 0.05 mm per 100 mm. The value on your order is set by your drawing, and we confirm in writing before quotation which features we can hold and which need a discussion.
Extruded or die-cast housing, which should I choose?
Extruded when the body is a constant section and the thermal path matters, because it is homogeneous, joint-free and cheaper to tool. Die-cast when the geometry is genuinely three-dimensional and cannot be closed by end caps. Porosity in a casting is the hidden variable; on a high-flux module seat it shows up as part-to-part scatter.
How do you reach IP67 or IP6K9K?
Through the end face, the cap and the fastening. The groove is machined to a controlled depth and the face is milled flat so compression is even, then the cap, gasket and screw torque are specified together. The rating belongs to the assembly, not to the extrusion alone, so we quote it against the full drawing.
Warum Harteloxieren statt normalem Eloxieren?
Because the housing is a high-voltage part and a structural part at the same time. Hard anodizing gives a thicker, denser film with better dielectric strength and much better wear resistance at the mounting faces. It is not a licence to ignore clearance, though: corners and threads need masking or distance.
Can you machine the water channel as a serpentine?
The channel inside the section is straight, because extrusion pulls a constant profile. A serpentine path is created by the end caps or by machining between passes, not by the die. If your drawing shows a true serpentine inside a one-piece body, that requires a different process and we will raise it rather than accept an impossible tolerance.
Führen Sie Dichtheitsprüfungen durch?
Yes, on water-cooled bodies, before coating. Testing after coating risks passing a part whose leak path has been sealed over by the film, which fails in the vehicle instead of at the bench.
Nächster Schritt
Send the housing drawing with the module seat, the sealing face and the coolant or airflow conditions. We will come back with a proposed section, a process route, and a written statement of what we can hold against your drawing.
E-Mail: linjunbing@truetrustlv.com | Anrufen oder WhatsApp: +86 136 6644 0600
ANGEBOT ERHALTEN
Sobald Sie Ihre Anforderungen übermittelt haben, kontaktieren wir Sie so schnell wie möglich bezüglich Ihrer Produktanfrage.:Kühlkörpergehäuse-Aluminiumprofil für Motorsteuerung